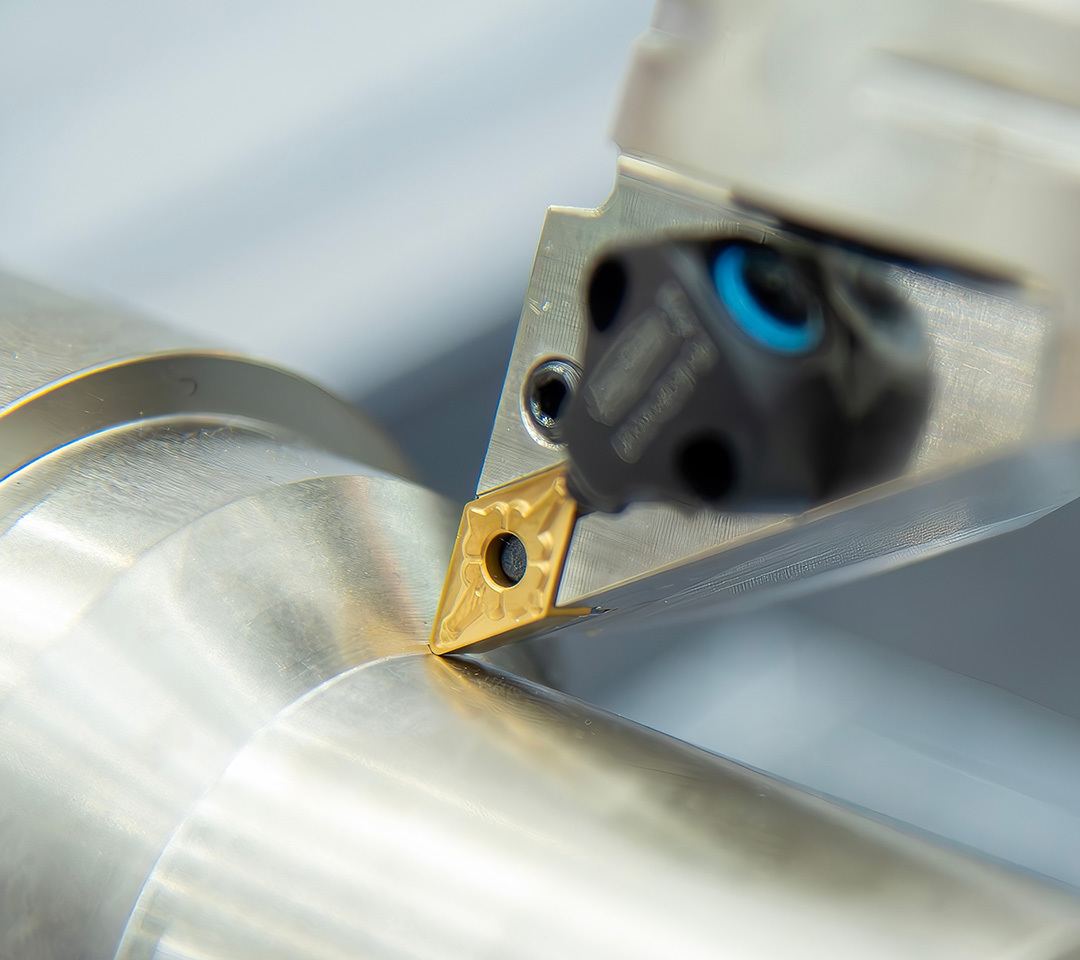
Eliminate Chip Entanglement and Abrasion! Achteck Launches New Integrated High-Pressure Through-Coolant Toolholder J Series of Small Parts for Stable Machining
Chip entanglement and rapid tool wear are long-standing challenges turning workshops in turning operations. Conventional external cooling fails to deliver coolant directly to the cutting zone. Swarf wraps around and scratches workpieces, inserts wear prematurely, and frequent tool changes lead to longer cycle times and higher machining costs.
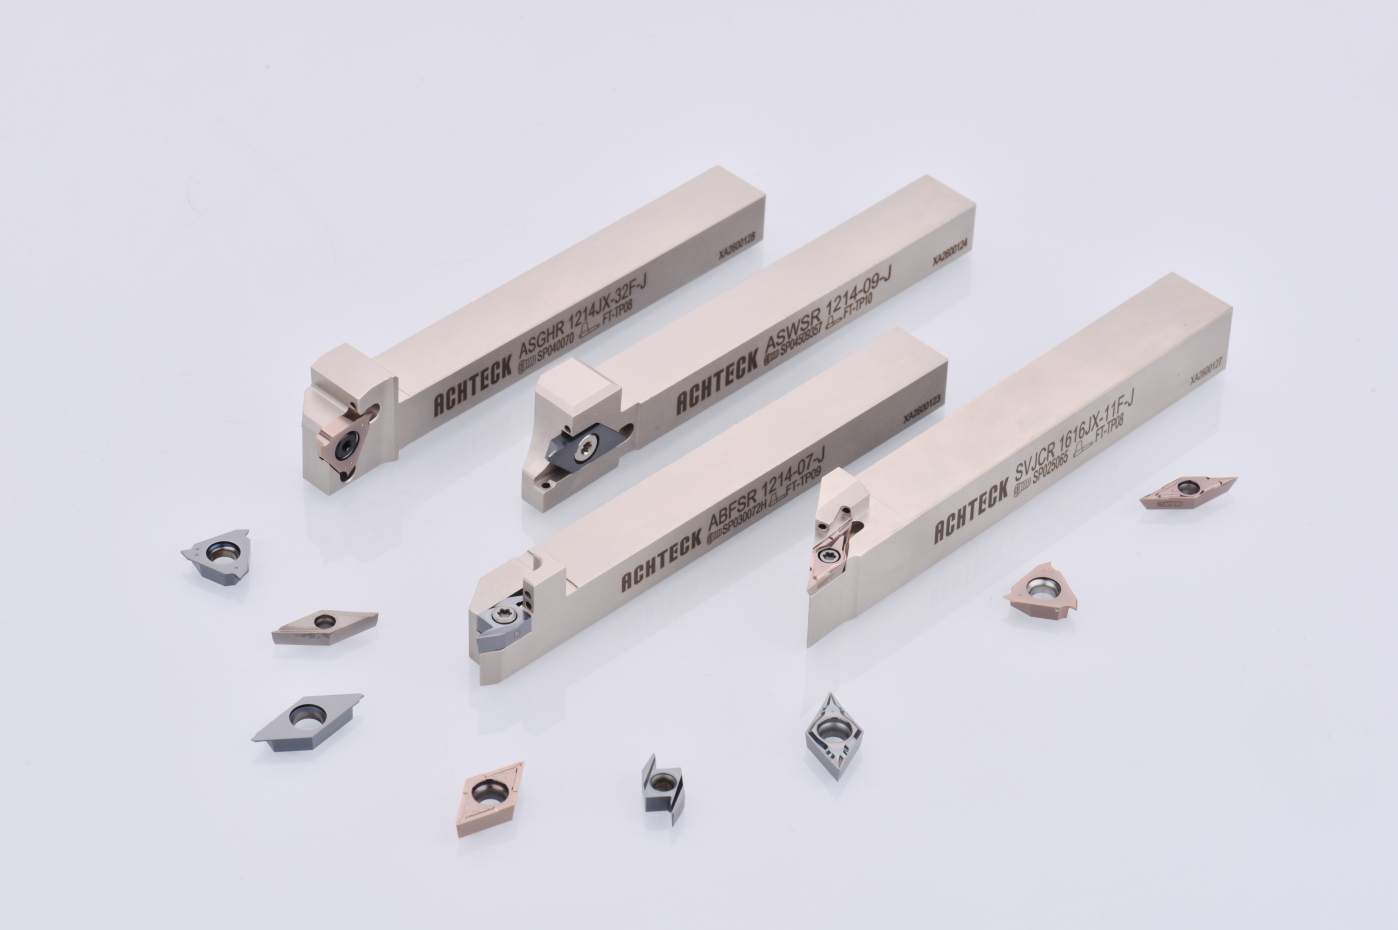
To address these pain points, Achteck is proud to introduce the new integrated high-pressure through-coolant toolholder J Series for small parts machining. Equipped with precision direct-spray cooling technology, it targets the heat source at the cutting point, efficiently breaks chips and suppresses tangling. It greatly improves turning stability for difficult-to-machine materials including 45# steel, titanium alloy and 316L stainless steel. The high-pressure direct jet hits the cutting edge directly, slowing tool wear substantially. Compared with standard cooling setups, it delivers a notable increase in tool life and provides reliable supports for high-speed, high-precision turning, making it the preferred solution for mid-to-high-end turning applications.
In today’s high-speed precision turning environment, cooling performance directly determines finished part quality and tooling costs. Achteck high-pressure coolant toolholders break the limitations of traditional external cooling, tackling chip wrapping and wear at the source. They balance productivity and cost reduction, delivering dependable cutting assurance for precision turning.
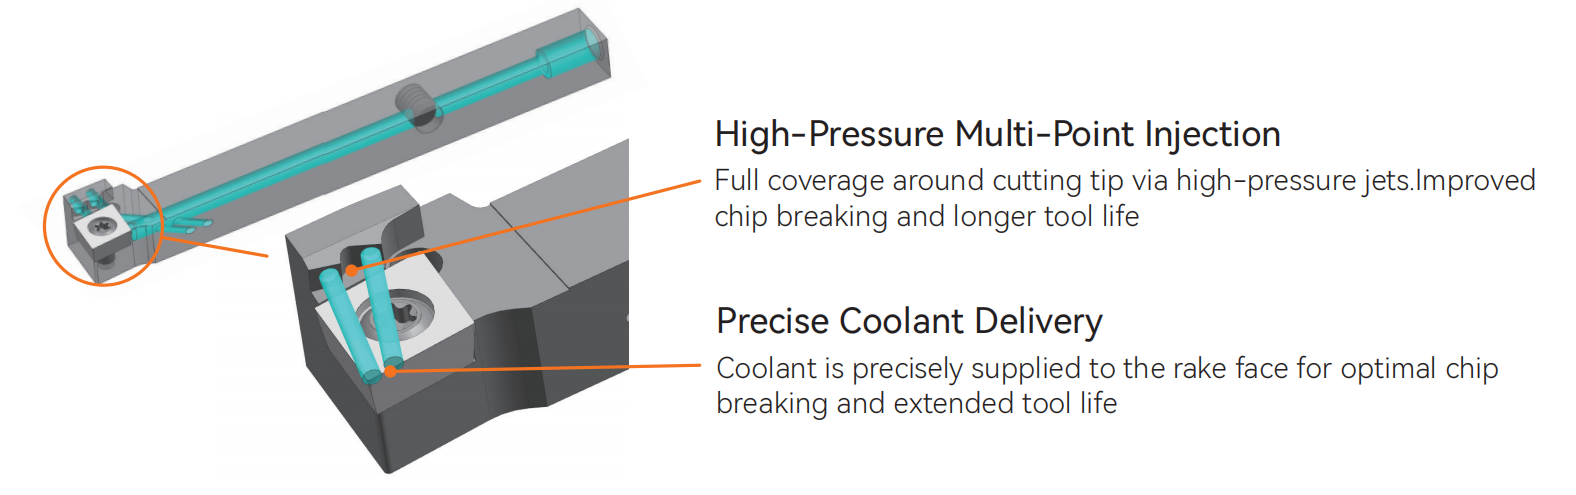
Excellent chip breaking capability for improved workpiece quality
Compatible with higher cutting parameters to boost machining efficiency
Superior cooling performance for extended tool life
⏩To prevent blockage of coolant outlets by swarf, filtration of the coolant is recommended.
Processes where chip entanglement causes non-conforming surface finishes
Processes where satisfactory chip breaking cannot be achieved solely by changing insert chipbreaker geometries
Processes with frequent cutting-edge thermal damage and high tool change frequency
Design Concep
Material: Titanium alloy
Params: S2000, f0.02, ap0.5 S2000 f0.02 ap0.5
Insert:XIN-DCGT11T308E-SF-A5956 AP100U
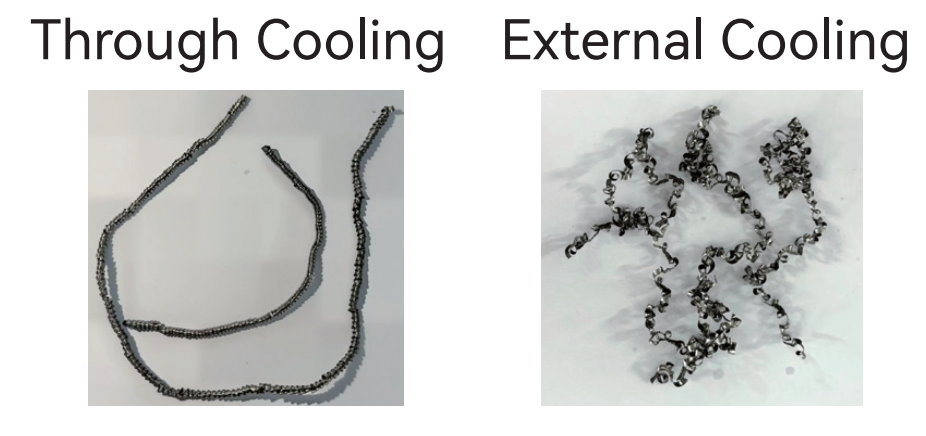
Controlled comparison under identical workpiece material, cutting parameters and insert specification: The new integrated high-pressure through-coolant toolholder J Series for small parts adopts direct coolant spray onto the cutting edge. Coolant is delivered straight to the high-temperature cutting zone, drastically enhancing chip breaking and fundamentally inhibiting chip tangling. It eliminates automatic line alarms and unplanned downtime caused by tangled chips, enabling stable long-duration unattended continuous machining while improving consistency and surface quality of finished parts.
Wear Resistance Comparison
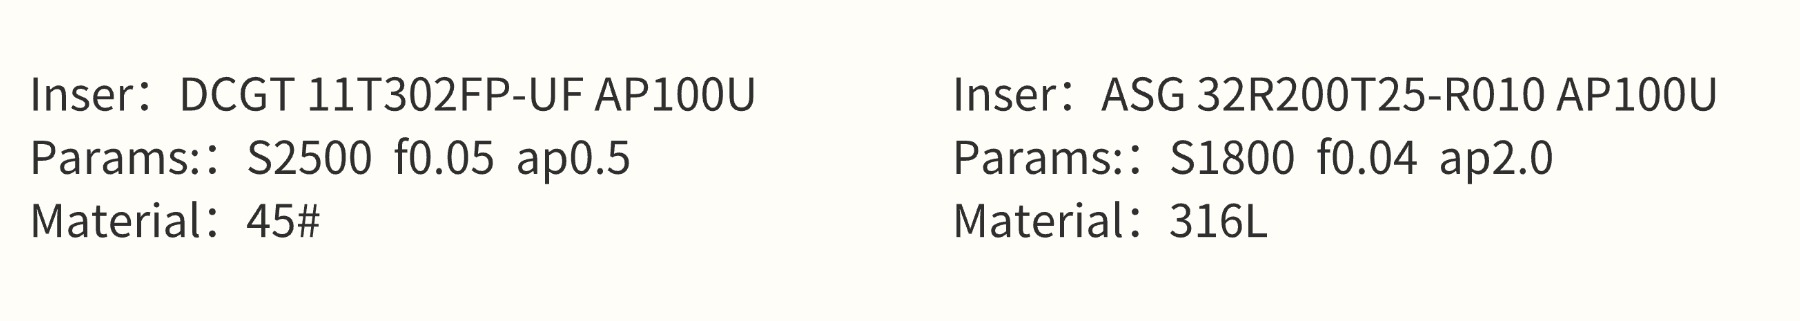
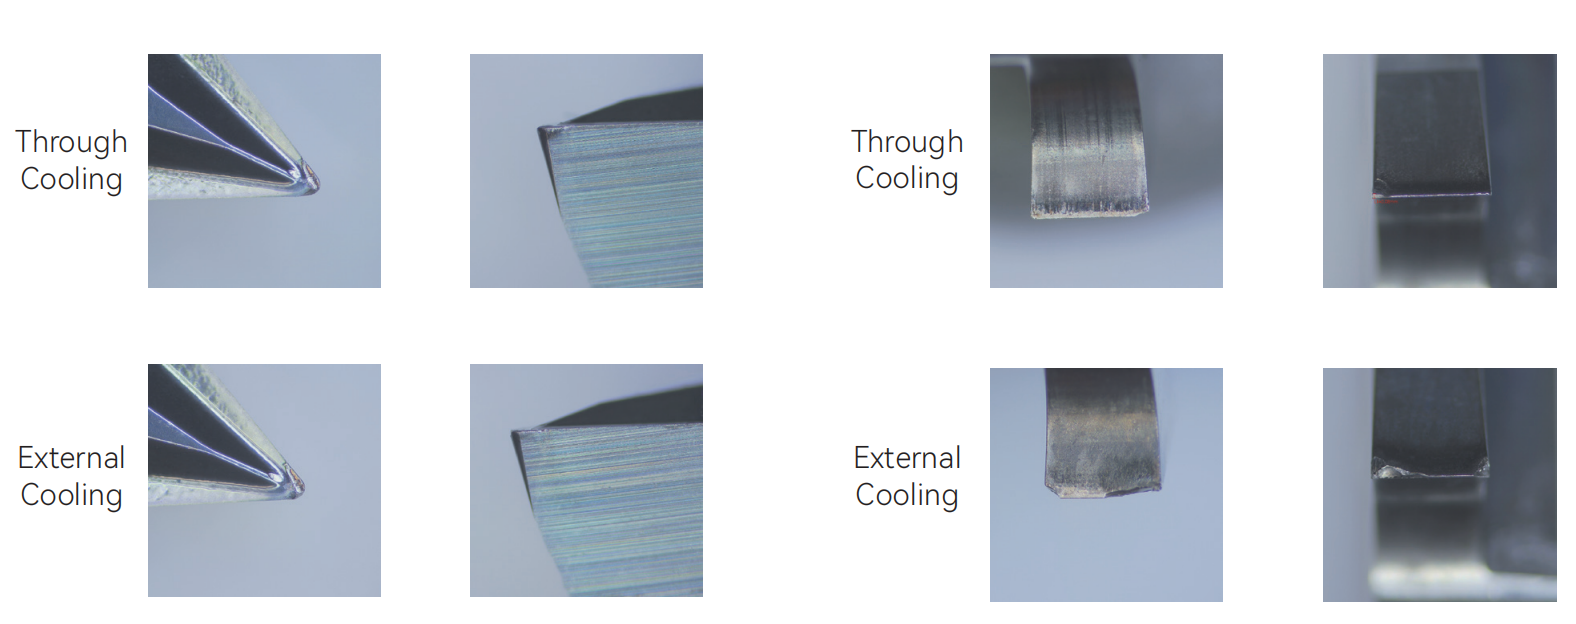
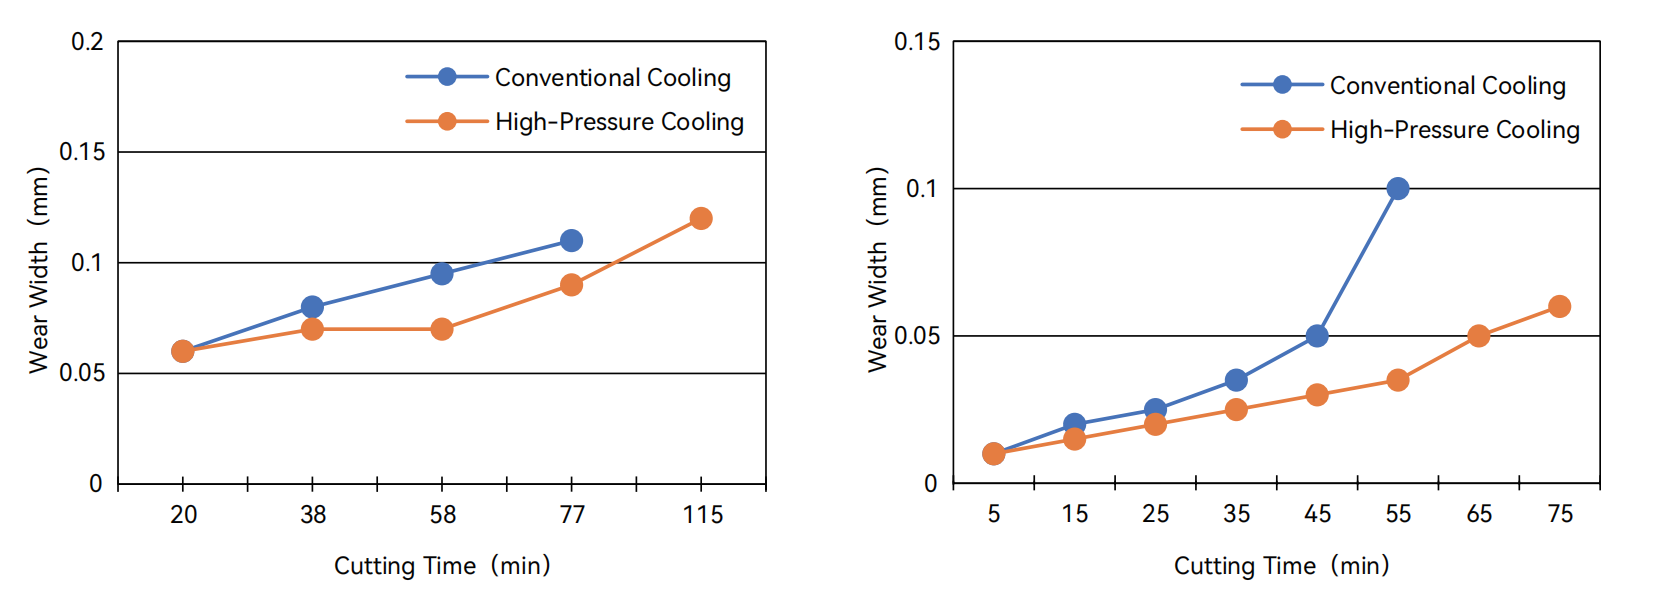
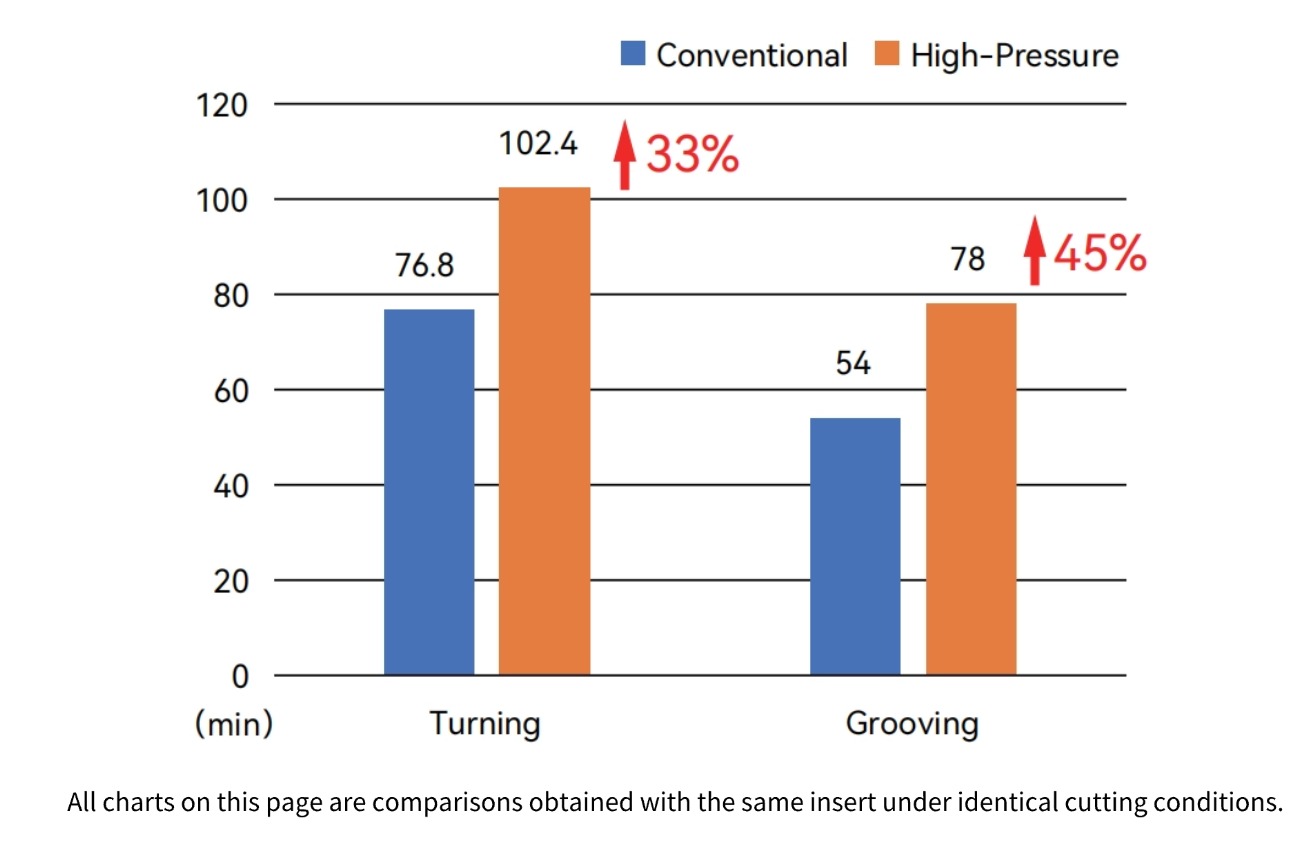
Under identical material, cutting parameters and insert configuration, the J Series effectively reduces thermal burning of the cutting edge, slows the rate of tool wear, extends insert service life and cuts tooling consumption costs.
Medical ultrasonic scalpel shafts are high-precision titanium alloy components widely recognised as difficult to machine. some of our medical-sector customers had long struggled with chip tangling during titanium alloy turning. Tangled swarf marred workpiece surface roughness, accelerated insert wear, raised tool change frequency, dragged down throughput and created severe capacity pressure.
Multiple process adjustments failed to fully meet on-site requirements, and the customer reached out to our technical team. We immediately launched cutting trials. After multiple rounds of testing, we confirmed that standard off-the-shelf chipbreaker geometries could not satisfy this application.
Our R&D team carried out targeted development and customised this high-pressure through-coolant toolholder, with repeated cutting tests focused on solving the industry-wide challenge of poor chip breaking in titanium alloy machining.
Field results were outstanding: stable chip curling and smooth evacuation were achieved for titanium alloy, eliminating chip wrapping on components. Workpiece surface quality remained consistent and controllable, and insert consumption dropped significantly. The trial performance won high recognition from the customer, who finally found a reliable solution to their long-standing titanium alloy machining bottleneck.
If you are facing poor chip breaking, chip entanglement or excessive tool consumption when machining titanium alloys, superalloys and other difficult-to-cut materials, please feel free to contact us. Share your workpiece material and process conditions, and we can provide custom cutting solutions and trial support.