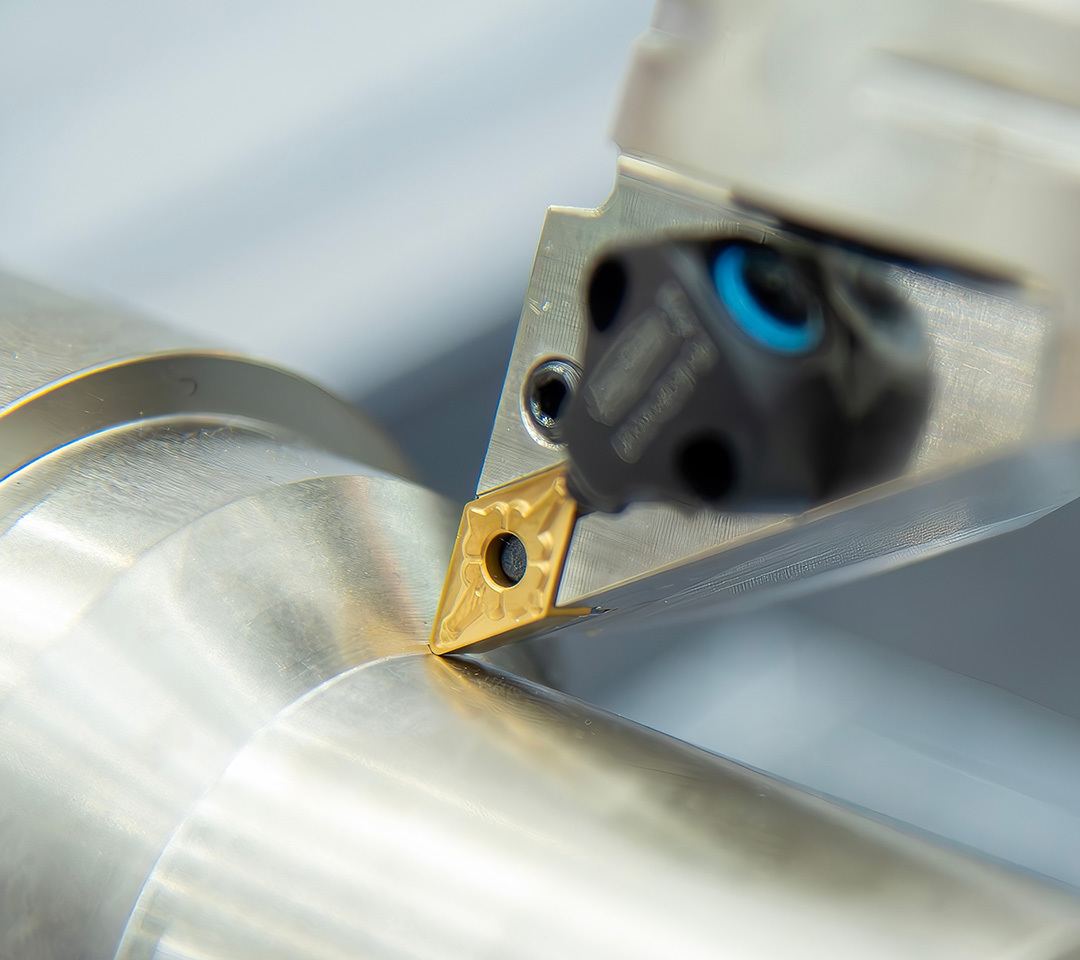
Cutters as Brushes, Craftsmanship as Ink | Achteck Tools Writes a New Chapter in the European Market
On September 15, AMB 2026–International Exhibition for Metal Working, Stuttgart in Germany. Following its appearance at EMO Hannover, this marks Achteck Tools' debut on the AMB stage. A range of innovative products and targeted machining solutions drew large numbers of professional visitors and industry customers from around the world to stop by for discussions — the technical appeal of a premium Chinese cutting tool brand continues to shine in the European market.
Responding to the core needs of global manufacturing, Achteck Tools has distilled years of technical expertise into specialized machining solutions covering four key industries — each market-proven and designed to address real industry pain points:
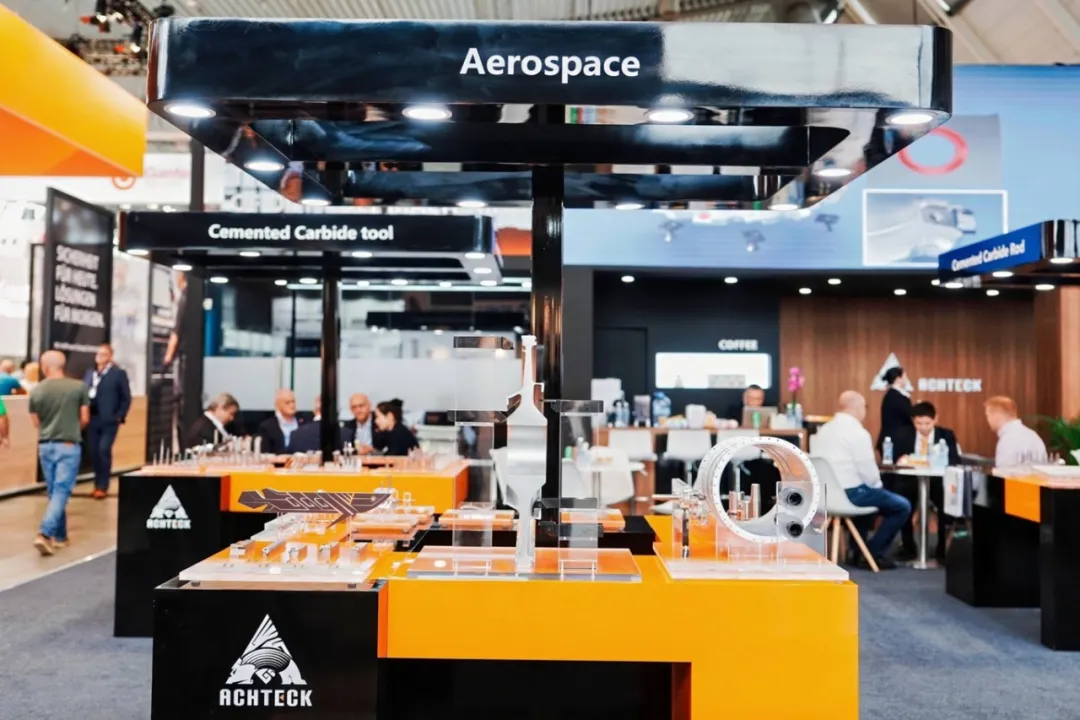
Landing gear, casings, blades, and complex blisk cavities — aerospace parts make extensive use of nickel-based alloys and titanium alloys, typically featuring deep cavities, thin walls, and high-precision geometries that impose near-exacting demands on process reliability. The machining challenges of these parts can rarely be solved by simply swapping an insert; they require a coordinated approach across machining programs, cutting strategies, process reliability, and clamping rigidity.
To address these pain points, Achteck Tools presented a range of matched tooling:
For blisk and blade profile milling, the APM00-RO series profile milling cutters, equipped with a newly developed proprietary PVD coating and available in MM3 and MR6 chip geometries — suited respectively to profiling semi-finishing and heavy-allowance roughing — deliver reliably extended tool life in superalloys and titanium alloys.
For casing and blisk ring-groove machining, the AROWANAG SERIES AP130S Grade for Diffcult-to-Machine Materlal Grooving combines a strengthened substrate with a purpose-built "wear-resistant outer layer, toughness-enhanced inner layer" coating, precisely solving the three major challenges of short tool life, uneven groove wear, and poor chip control when grooving superalloys. Multiple chip geometries — CS/CM, TS/GS, and RM/RS — cover general external grooves, complex-profile ring grooves, and seal grooves.
For face milling, shoulder milling, and slot milling of titanium structural parts, the AP351S grade tackles chip adhesion and poor thermal conductivity, balancing milling efficiency with durability.
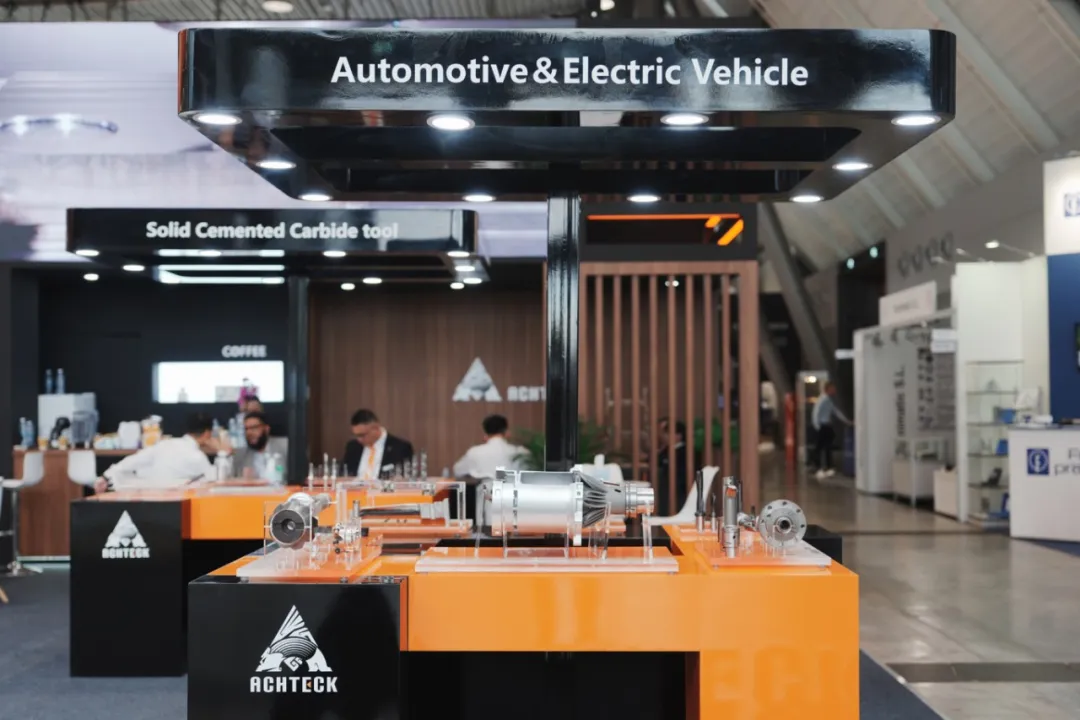
Crankshafts, camshafts, valve seat rings, brake discs, cylinder blocks, transmission housings, and aluminum NEV subframes — the challenge in automotive part machining has never been "can it be done," but cycle time and cost per part. On the same production line, a small gain in efficiency and tool life adds up to a substantial cost difference over the year.
At this show, Achteck's automotive solutions cover both conventional and new-energy applications: for hardened steel and cast iron critical parts, the "hard turning instead of grinding" approach uses PCBN turning inserts to finish crankshafts, camshafts, valve seat rings, and brake discs in a single setup — eliminating downstream grinding operations and workpiece handling entirely. For high-volume structural parts such as cylinder blocks and transmission housings, the AO series multifunctional shoulder milling cutters feature helical progressive cutting edges that build radial force gradually, ensuring smooth entry and light cutting while handling both face milling and right-angle corner cleanup — helping high-volume lines bring unit costs firmly under control.
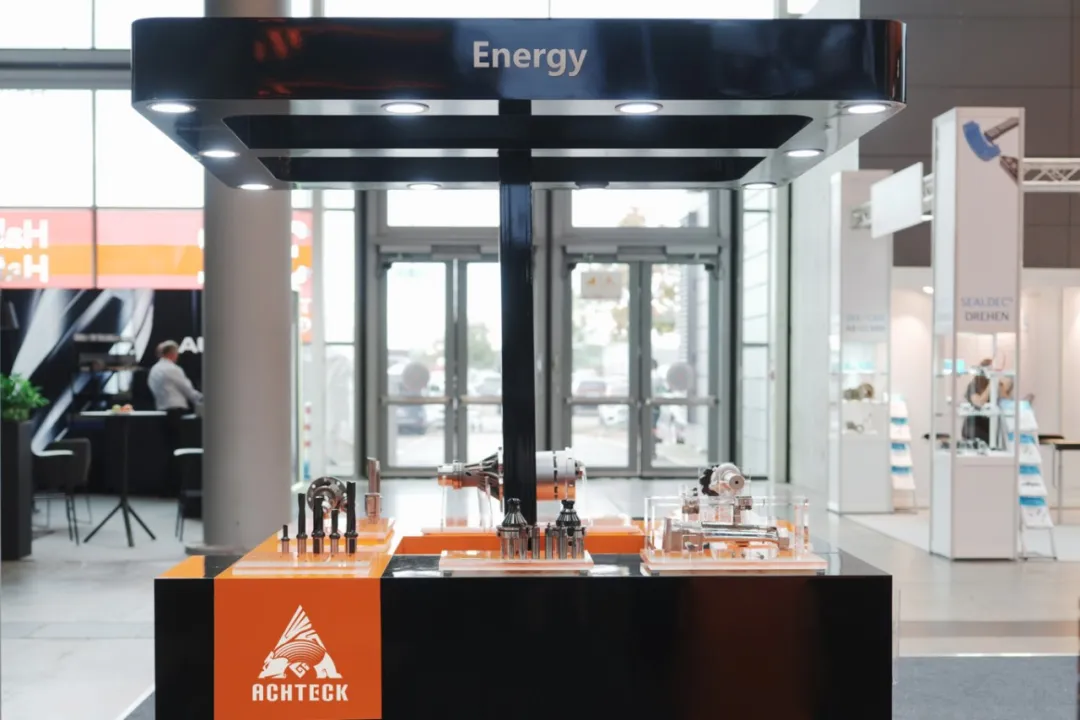
Turbine rotors, wind turbine hubs and gears, and oil & gas equipment pipe fittings — these core energy components are typically large, feature deep cavities, and require long machining cycles. Line downtime is extremely costly, and losses from unexpected tool failure far exceed the cost of the insert itself.
For these heavy-duty machining scenarios, Achteck offers a range of matched tooling: round-insert milling cutters and slot milling cutters for turbine blade and rotor groove machining, meeting the demands of continuous, long-cycle deep-slot cutting; the AO series shoulder milling cutters paired with indexable short-hole drills handle milling and holemaking on large wind power and oil & gas components. This short-hole drill delivers a high metal removal rate and outstanding efficiency, with advanced manufacturing and inspection equipment ensuring batch-to-batch consistency. Simply replacing the insert clamping screws at regular intervals extends drill body life and reduces cost per hole; switching insert grades adapts the tool to multi-material, small-batch flexible manufacturing, while the insert end can be continuously upgraded with the latest coating technology to tailor high-volume solutions — helping customers hold quality and control costs in large-part machining.
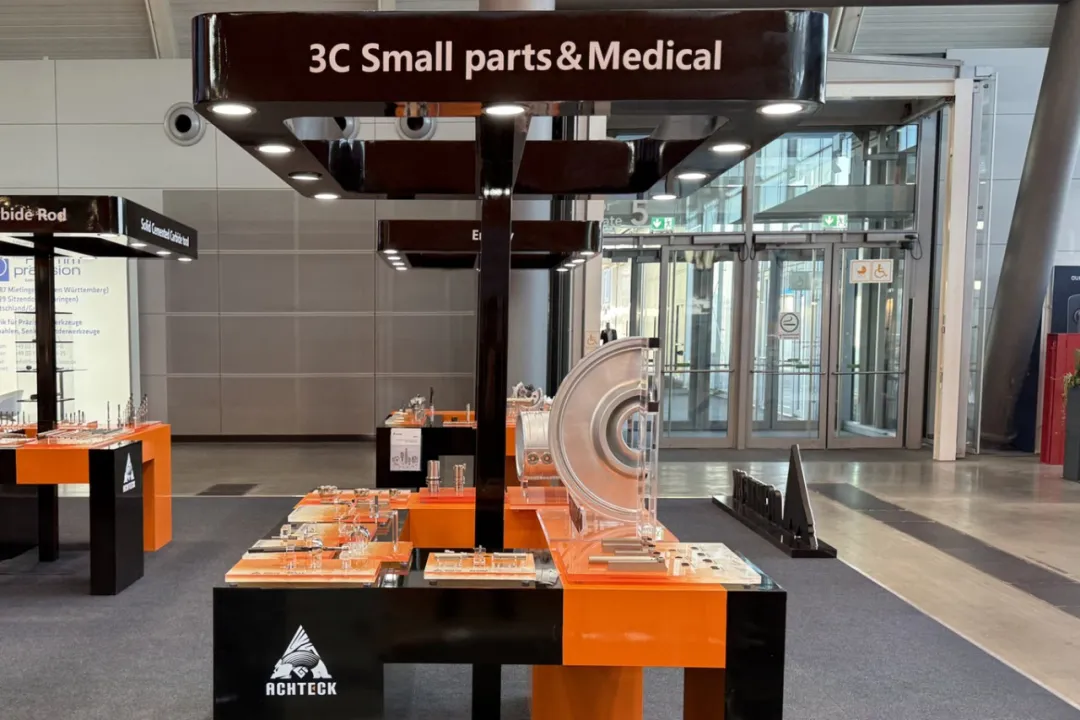
Lens rings, watch cases, sensor components, hydraulic valve parts, quick-connect fittings, and medical bone screws and plates — these parts are small, tightly toleranced, and produced in high volumes. What customers must balance is never a single-operation challenge, but the triple requirement of dimensional accuracy, production cycle time, and sustained delivery.
For precision small-part machining, Achteck presented a turning tool portfolio covering the core operations: external turning tools, profiling turning tools, small-diameter boring bars, shallow grooving tools, and back turning tools. At the heart of the lineup is the flagship AP100U grade: an ultrafine tungsten carbide substrate with high hardness, combined with a nano-multilayer alternating composite coating and an ultra-smooth surface finish. The finely ground cutting edge is sharp, with excellent red hardness and thermal stability, while the low-friction surface effectively suppresses chip adhesion and workpiece surface scratching. Longer and more consistent tool life not only reduces downtime for tool changes, but also prevents dimensional drift and surface rework caused by edge wear in volume production — enabling customers to hold both yield and delivery pace in high-precision small parts such as lens rings, watch cases, and bone screws and plates.
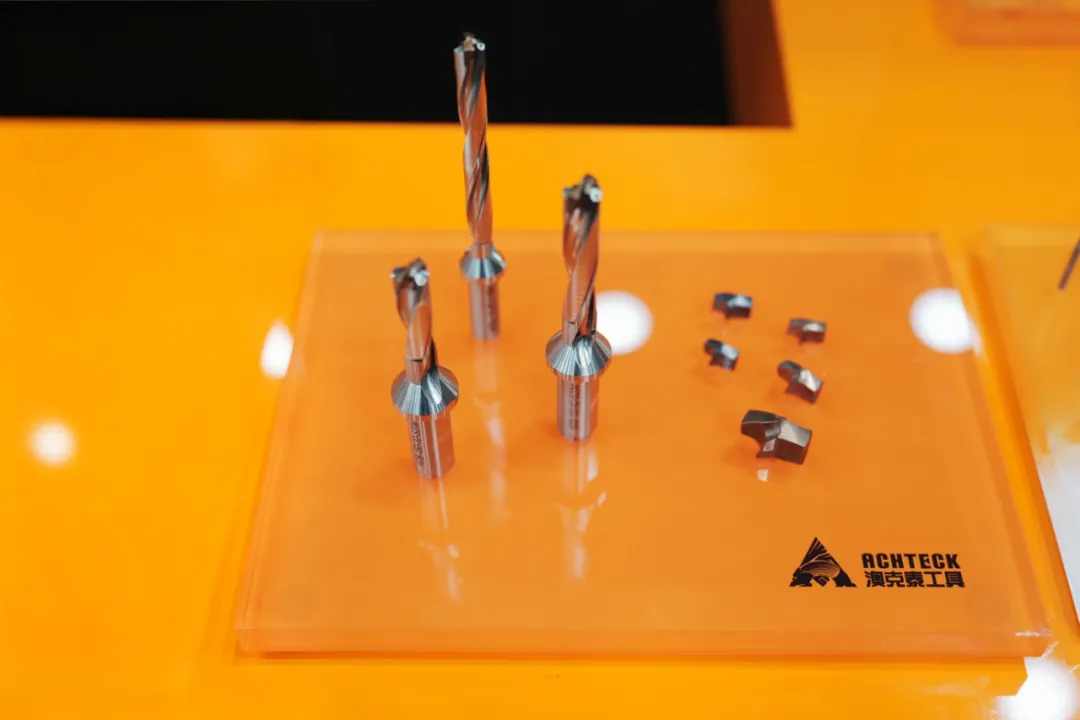
D190 modular drill : drill holder accommodates multiple drill heads for different working conditions; the high-rigidity body ensures stable drilling accuracy; the crown drill tip can be reground and reused multiple times, effectively reducing cost per hole.
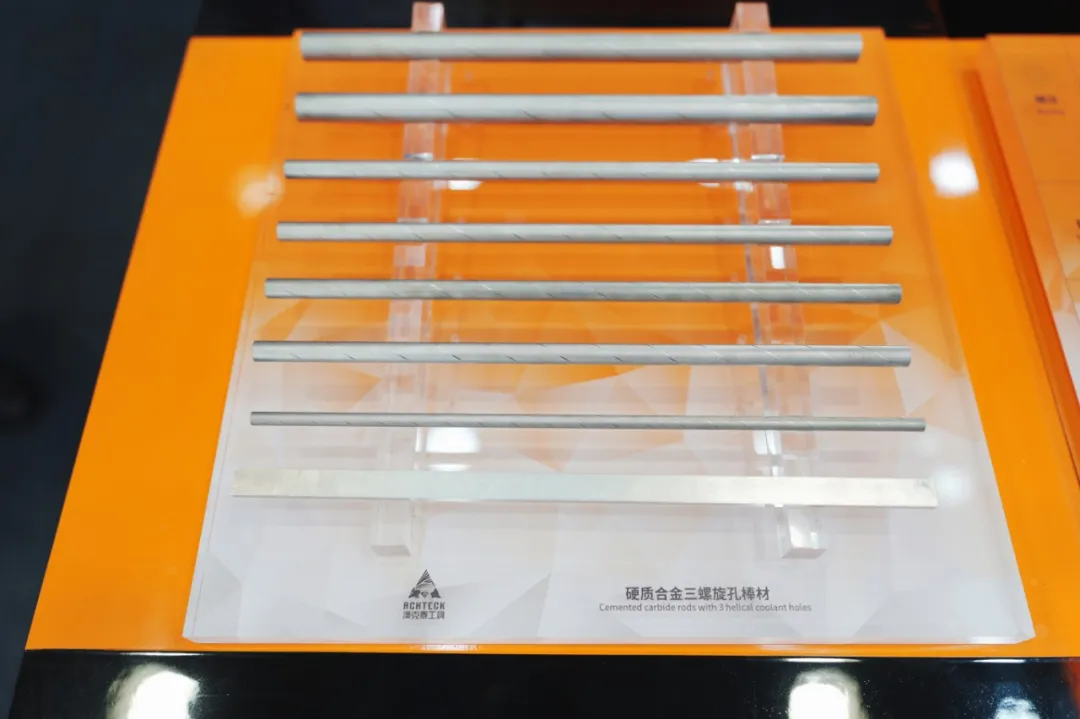
Cemented carbide rods: independently developed and manufactured by Achteck Tools, covering the three major forming processes — die pressing, extrusion, and dry-bag isostatic pressing — with specifications ranging from micro to extra-large diameters, solid to coolant-hole designs. Backed by a fully in-house production chain from substrate formulation to finished tools, Achteck delivers consistent quality, controllable lead times, and rapid response to customization needs.
In-Depth Exchanges
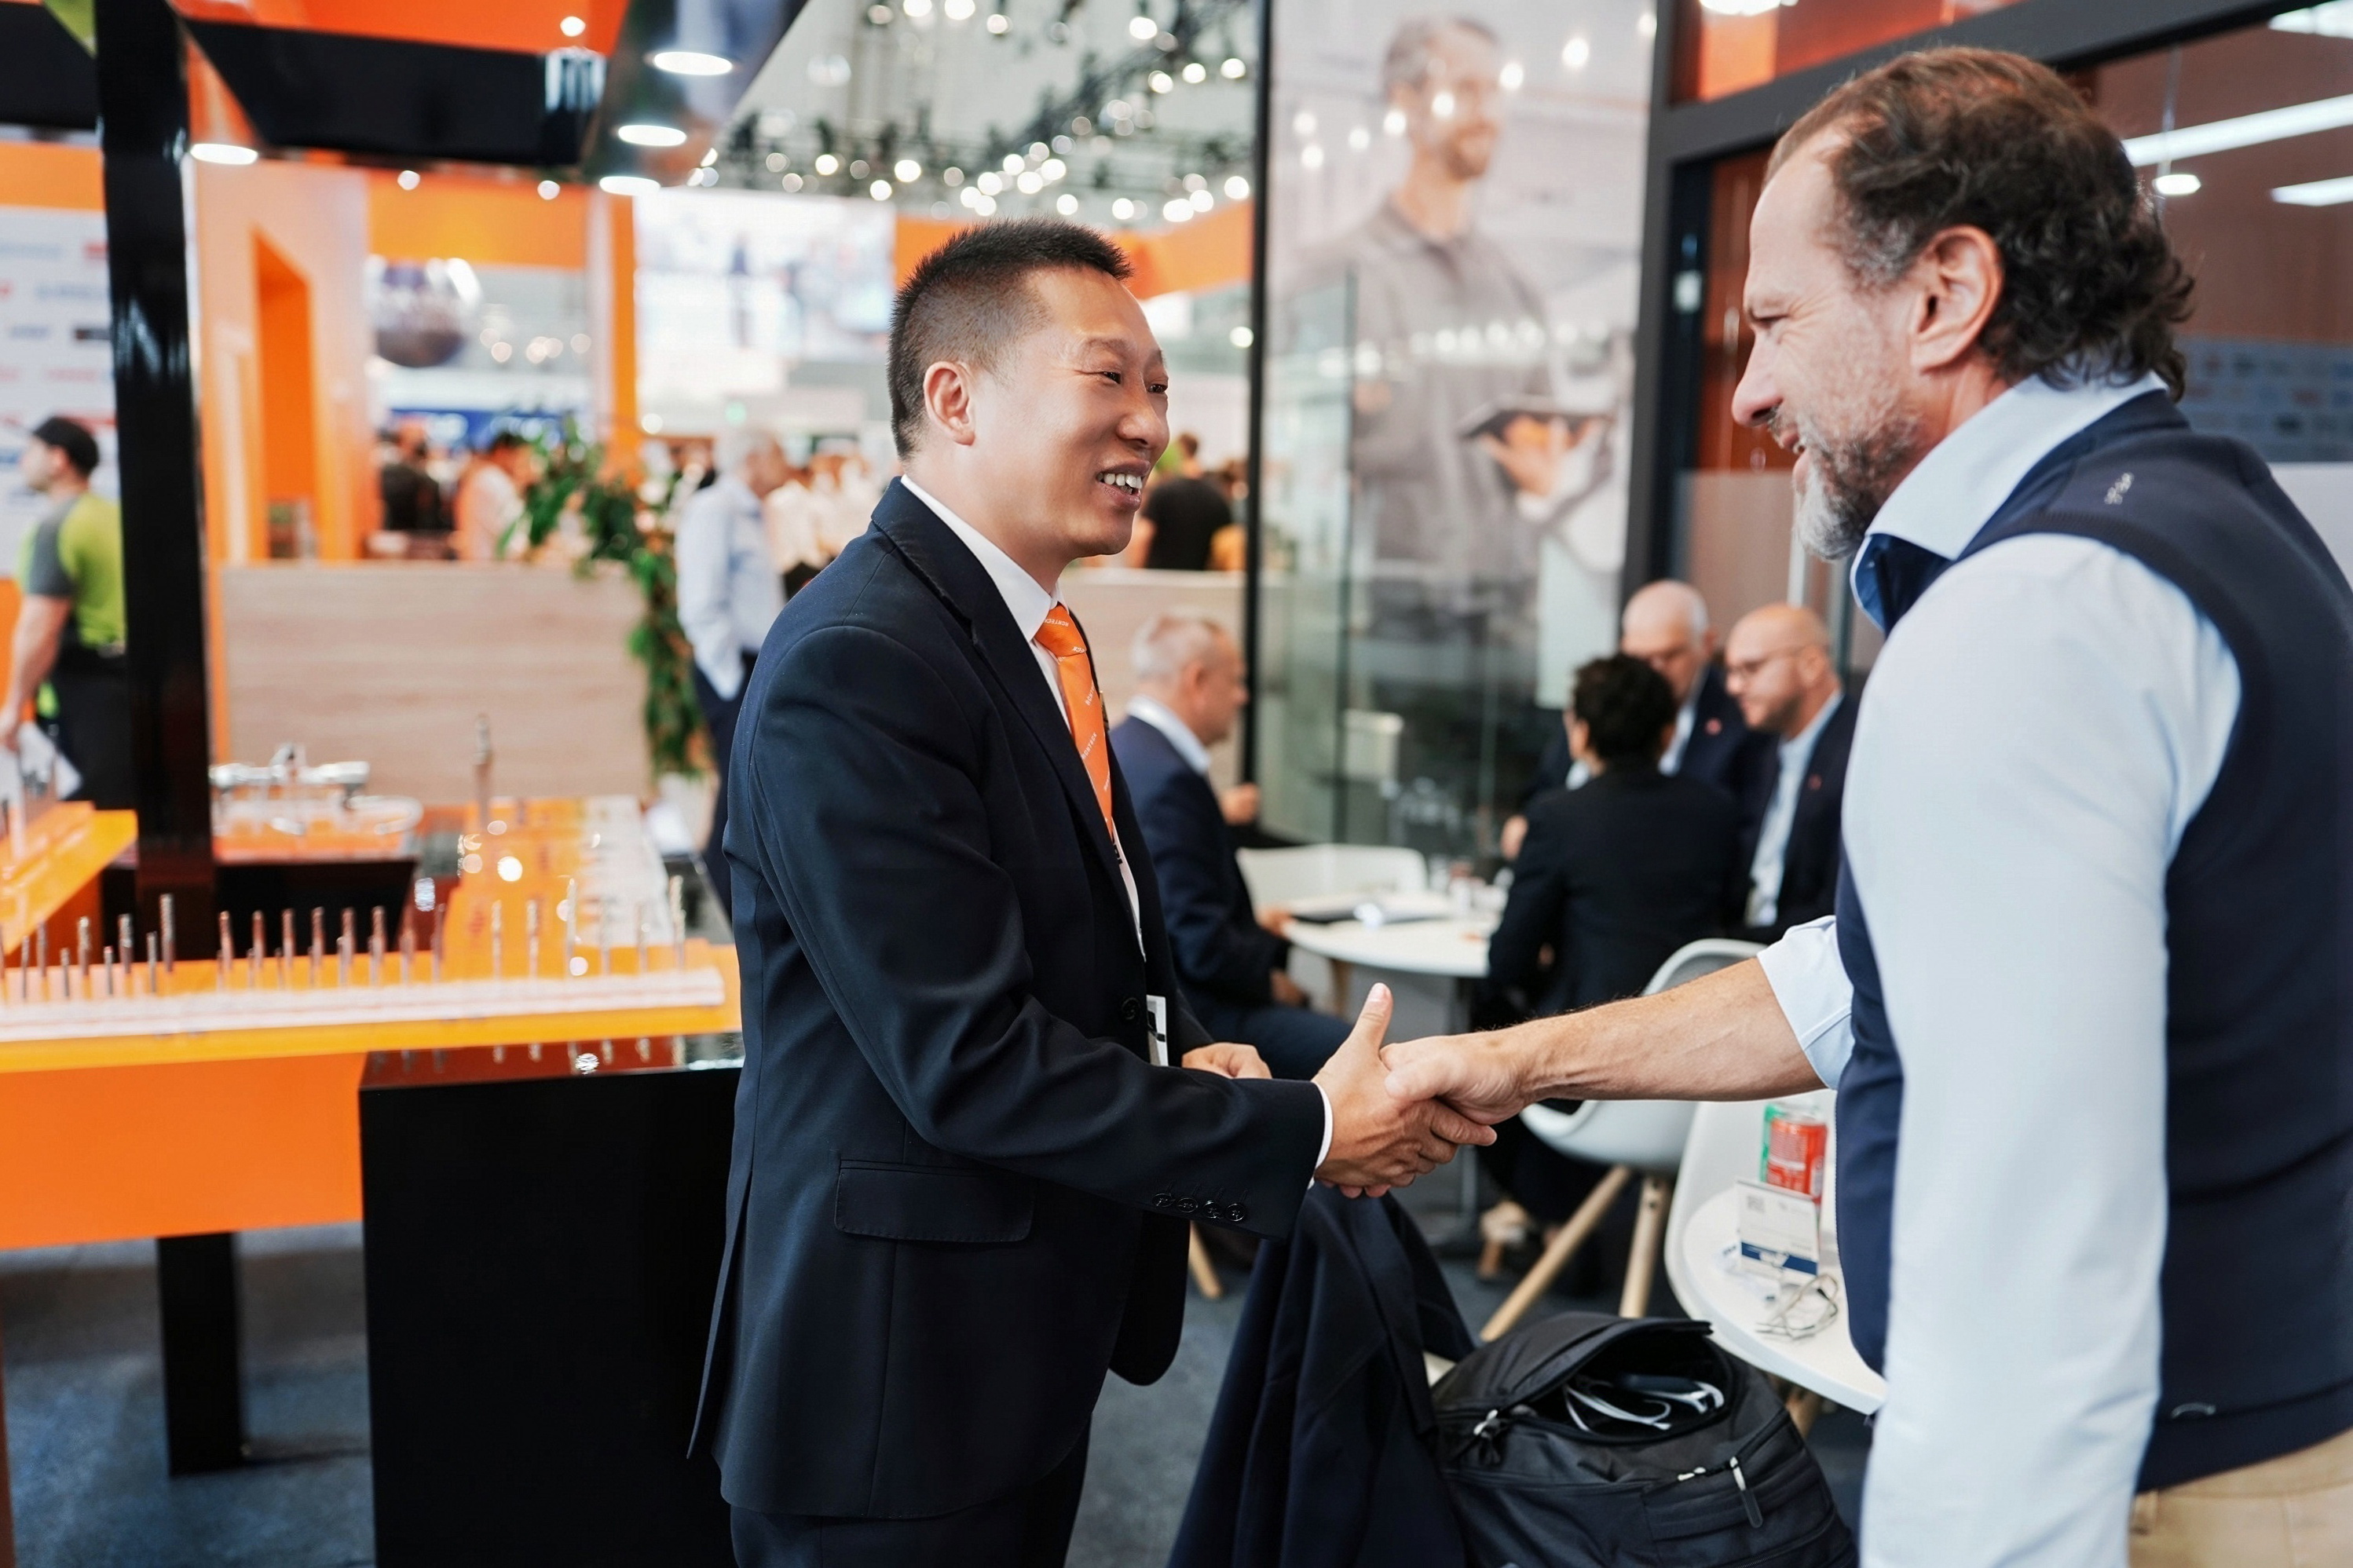
During the exhibition, the booth welcomed professional visitors from across Europe and many other countries and regions. Beyond product and technology exchanges, Achteck's application engineering team provided on-site, in-depth technical services — including machining process analysis, tool selection advice, and cost-reduction assessments.
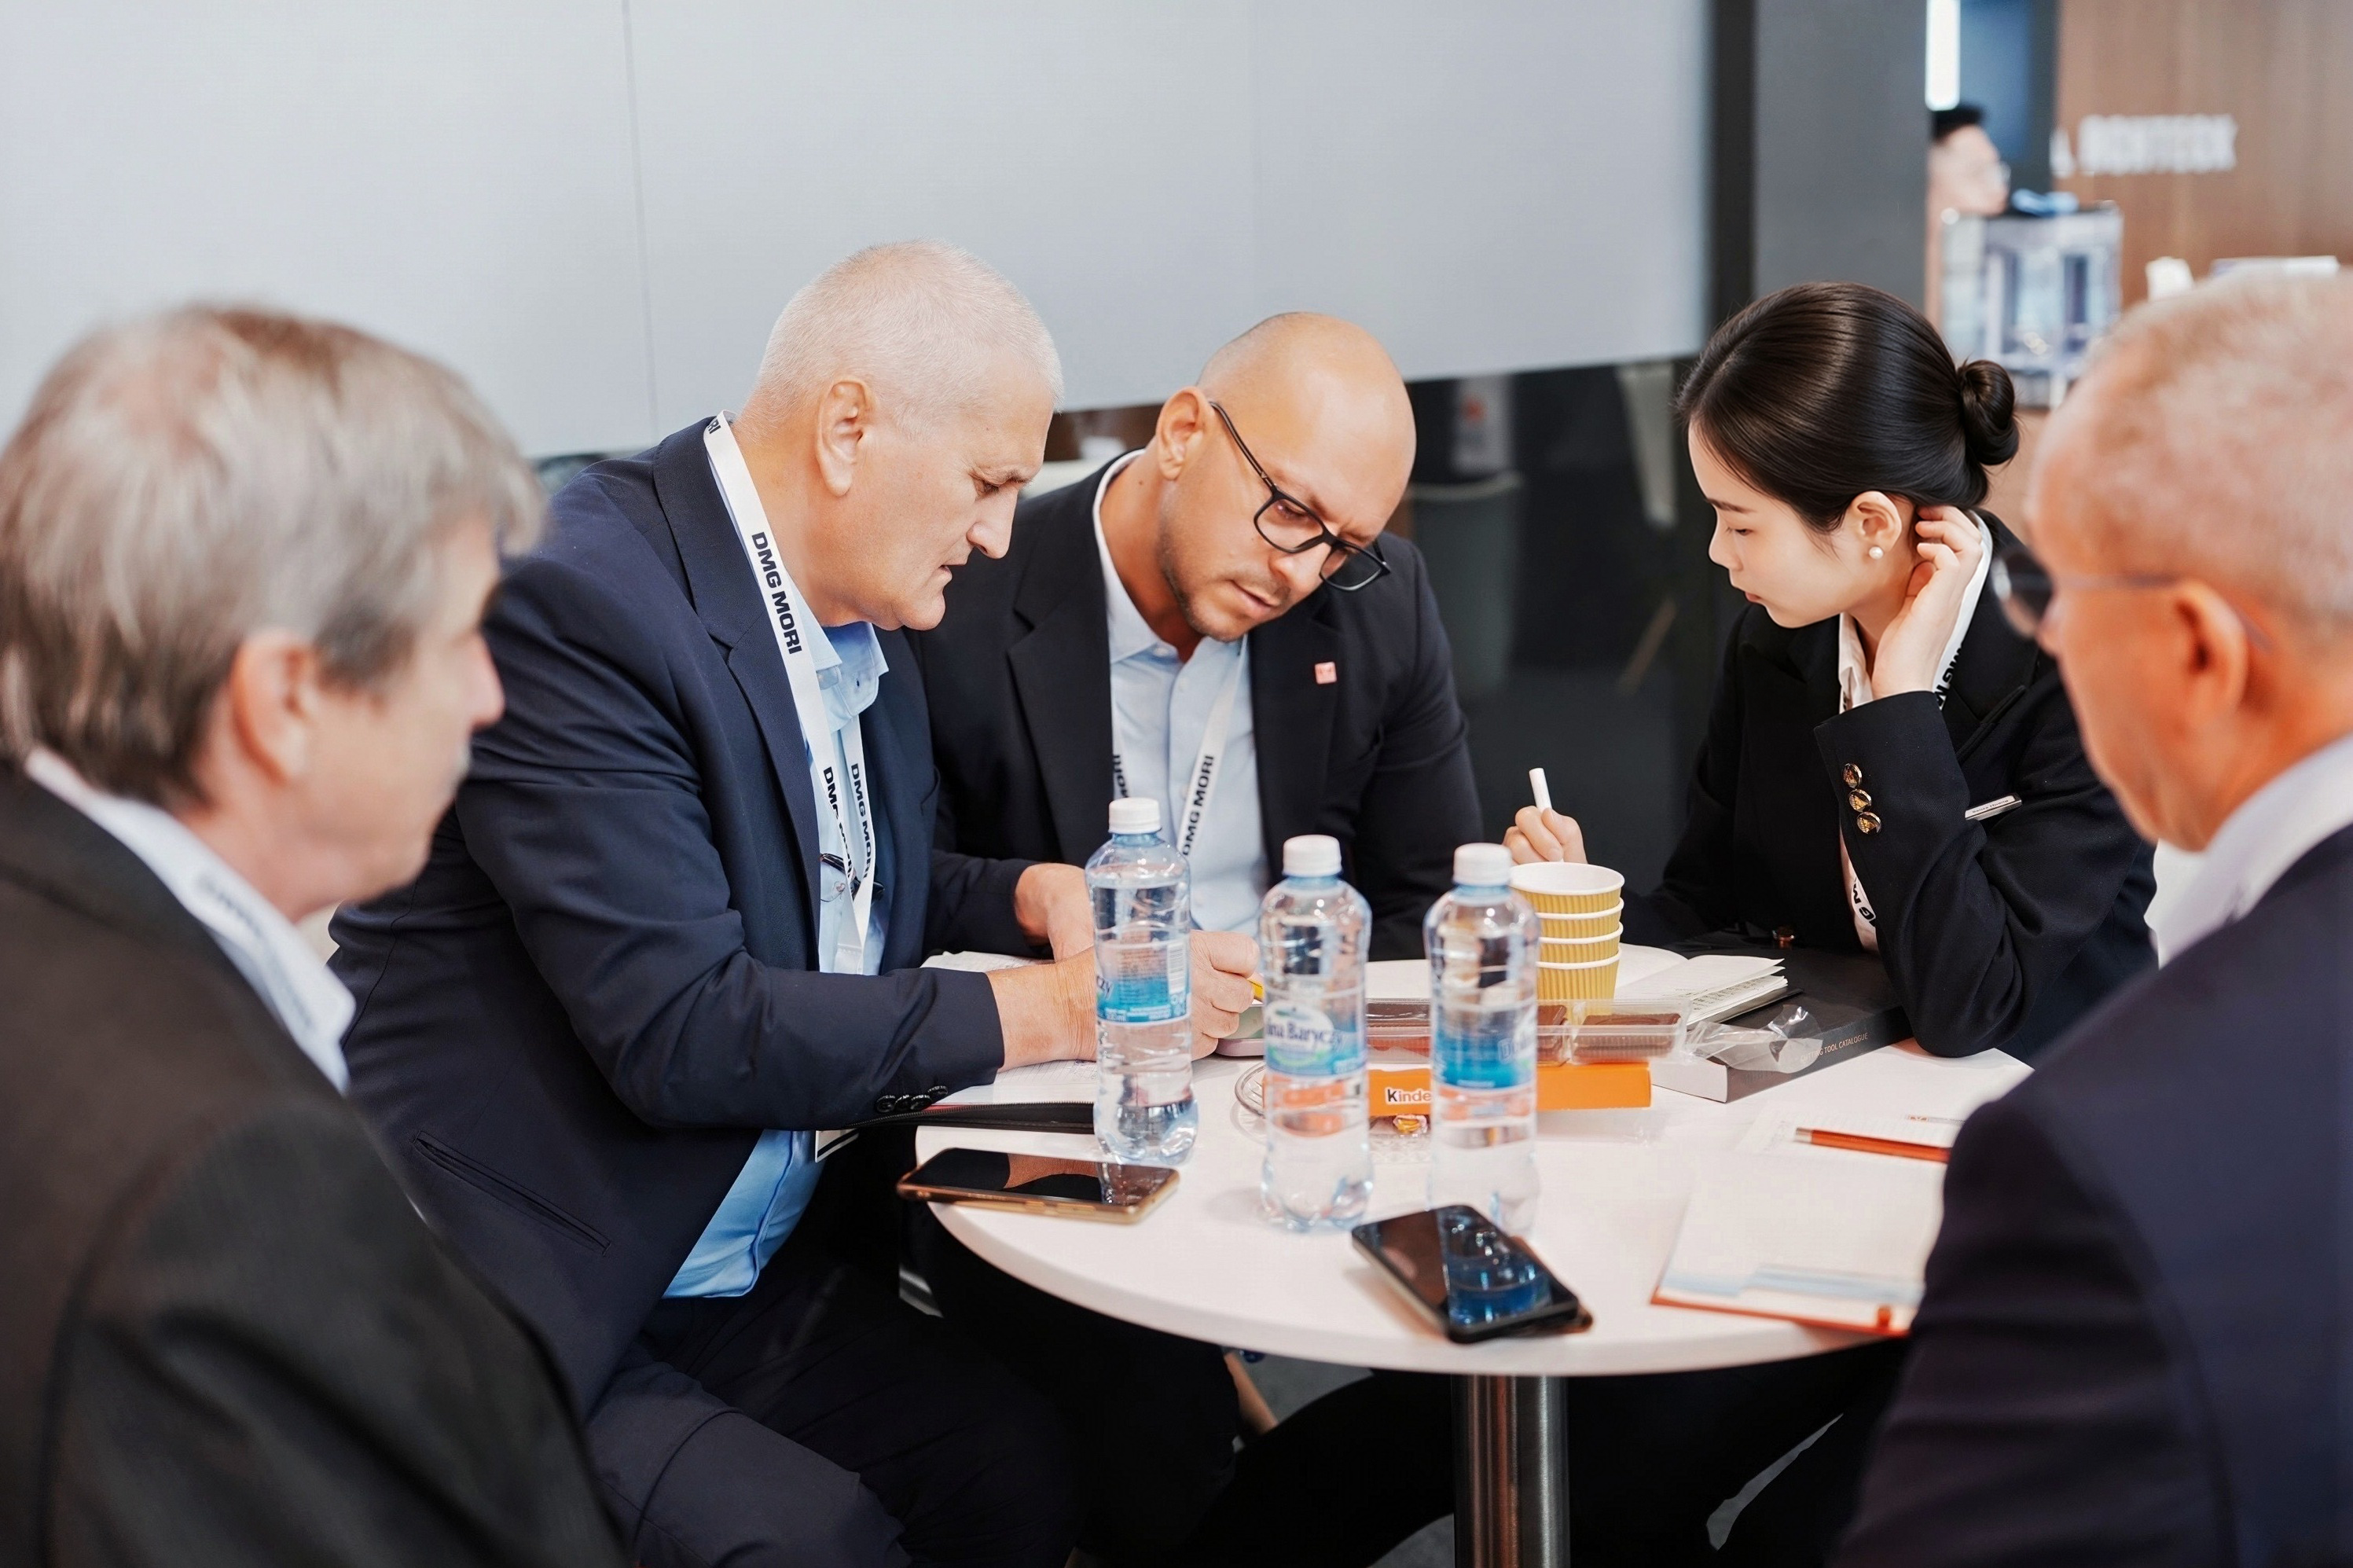
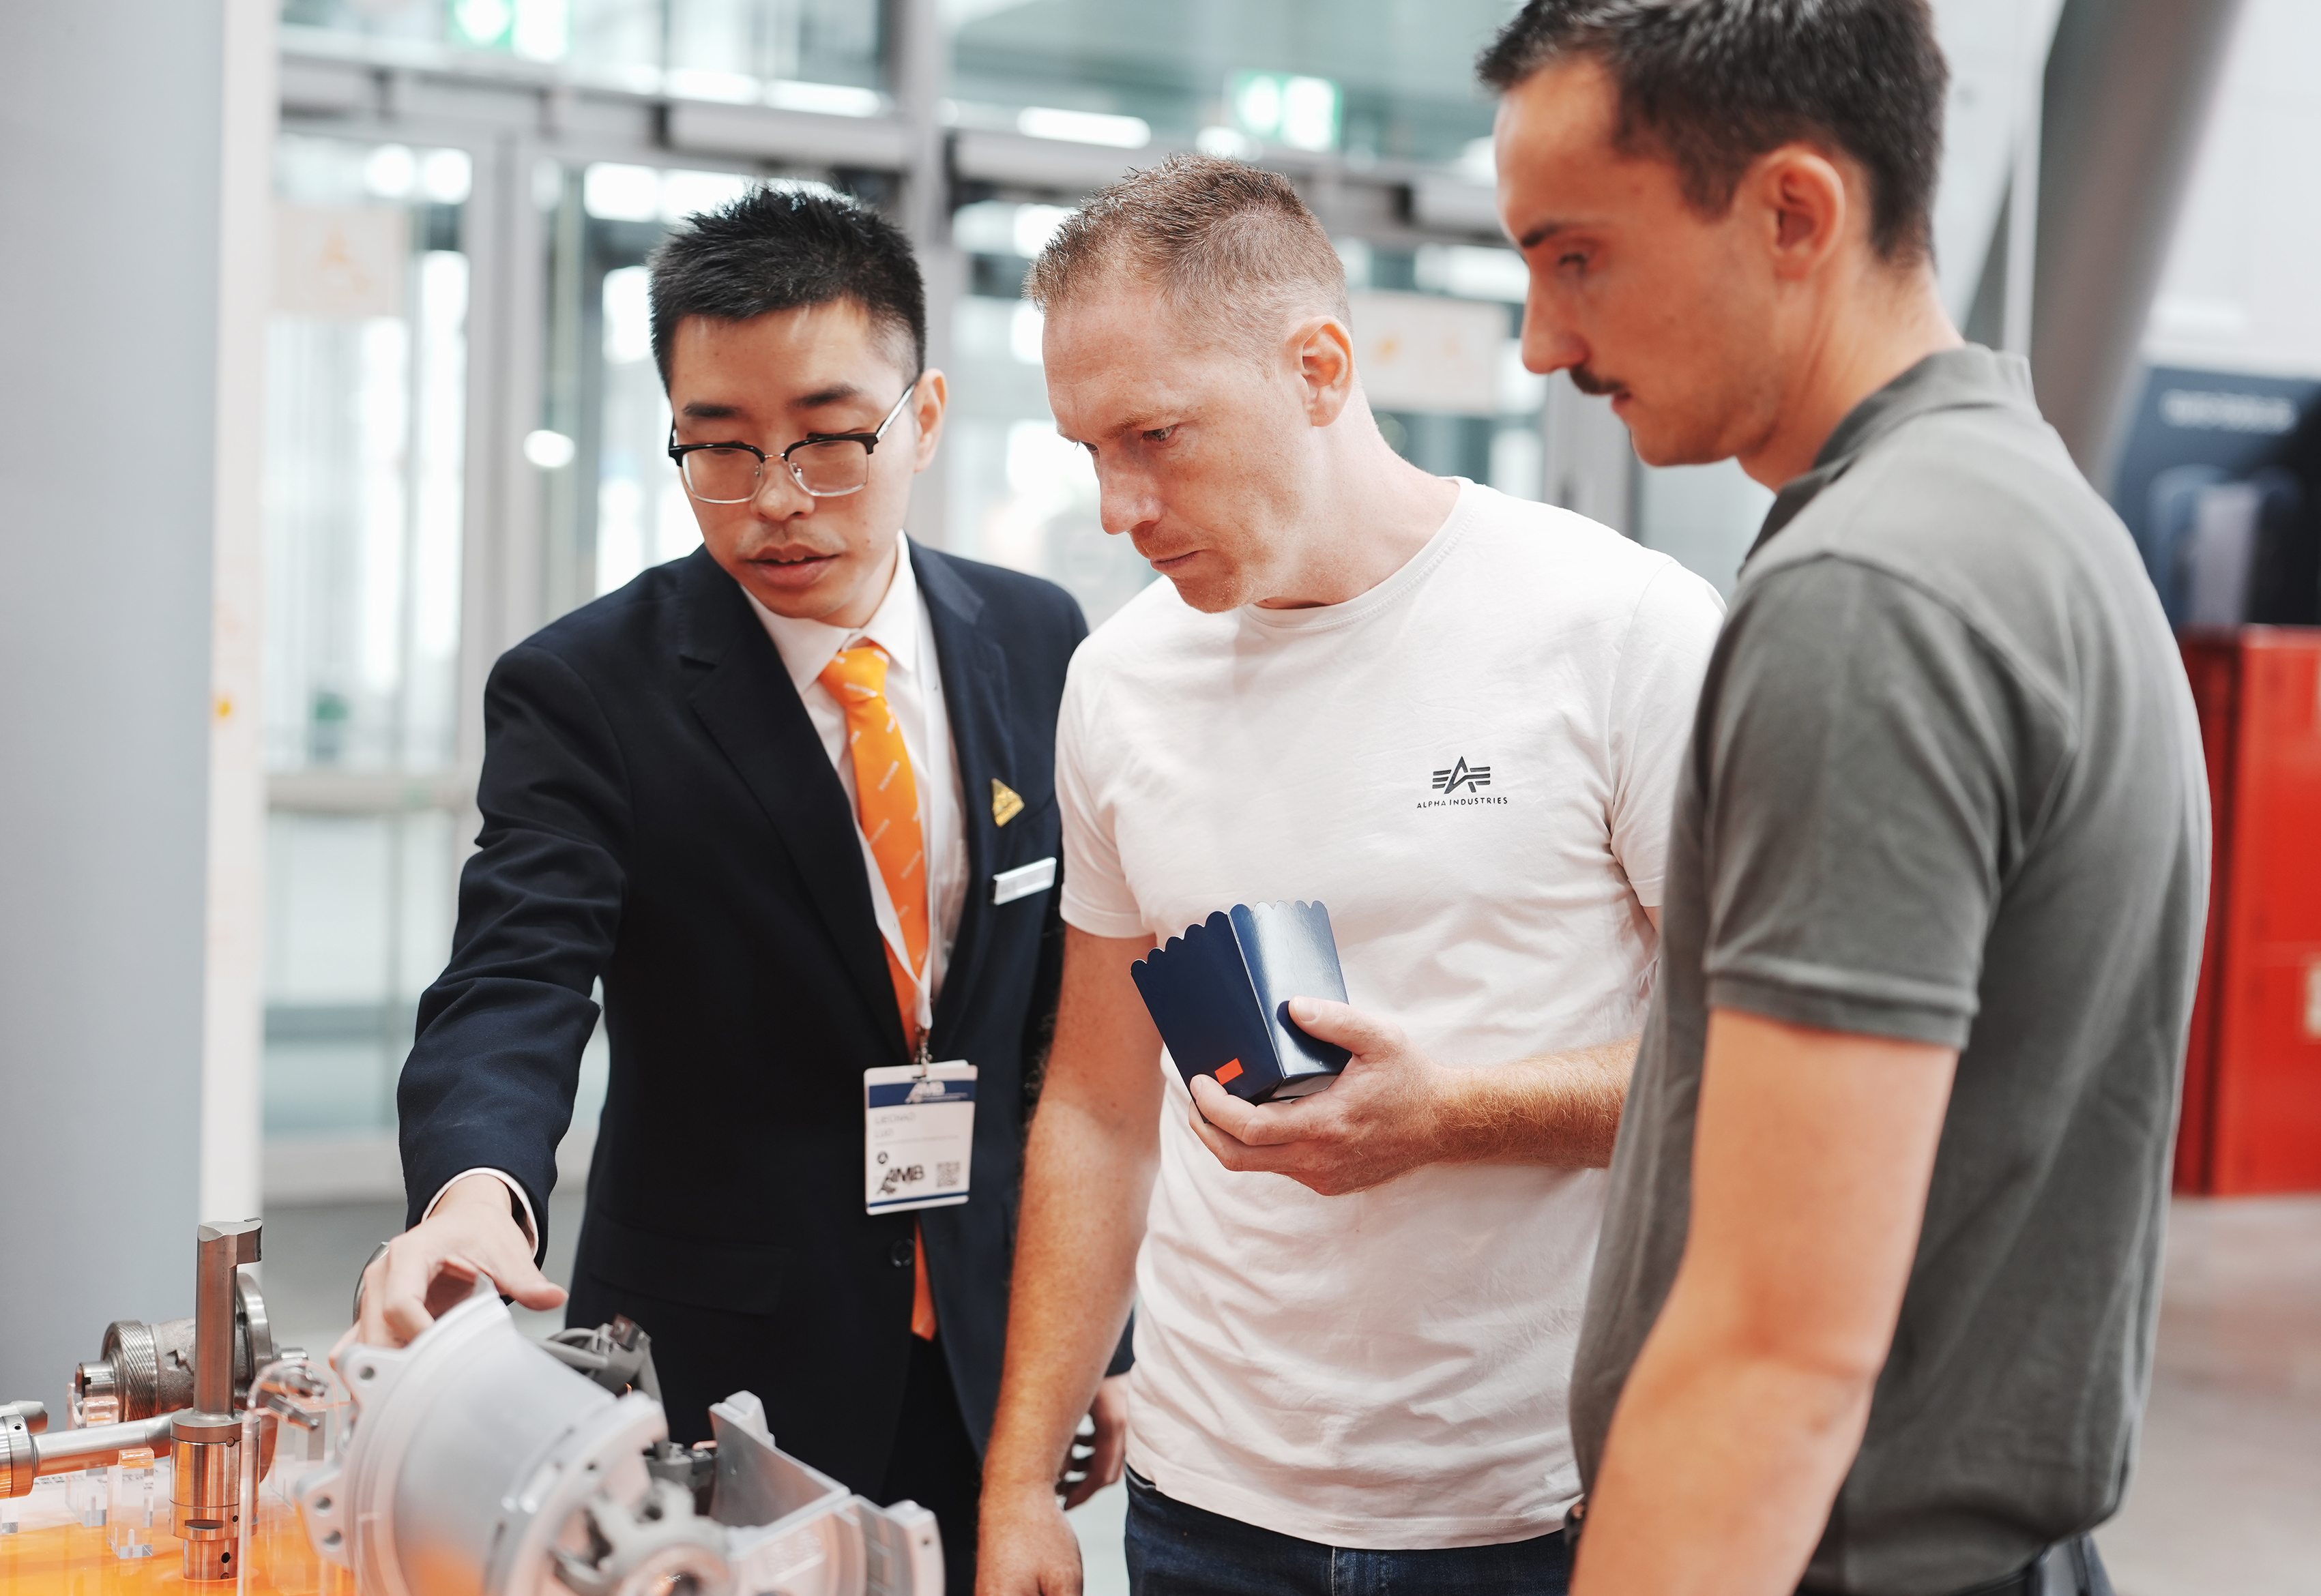
Several long-standing distribution partners made special trips to the booth for in-depth discussions on next year's product line planning and market coordination. Many first-time visitors, after learning in detail about the products and machining case studies, left specific machining requirements and arranged for post-show technical follow-ups. Professional conversations centered on specific materials, specific parts, and specific parameters became the main theme of the booth's exchanges.
Deepening Roots in Europe
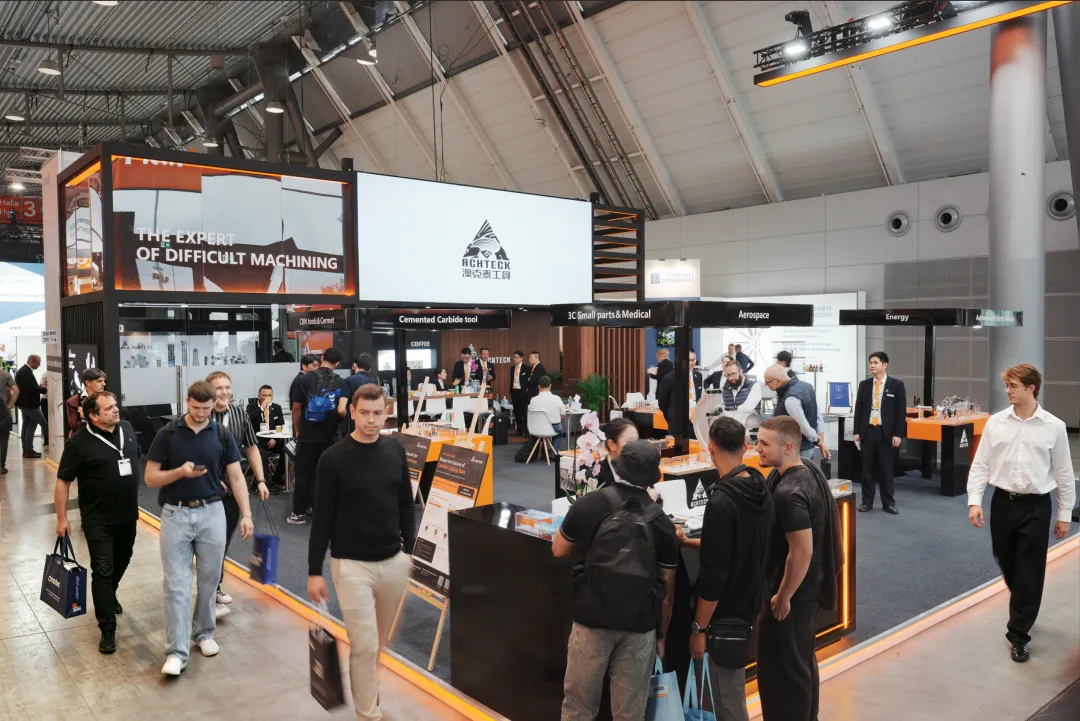
Demand for machining difficult-to-cut materials in the European market continues to grow. Taking aerospace as an example: lightweighting and emissions-reduction goals are driving a rapid rise in the use of titanium alloys and other difficult-to-machine materials, while fast tool wear and high machining costs are real pain points for local manufacturers. This aligns closely with Achteck Tools' long-standing areas of focus.
From EMO to AMB, Achteck Tools' internationalization path is clear and determined: not only bringing products to the European market, but rooting technical services in Europe and deeply integrating total solutions into customers' production lines. Relying on the full-industry-chain advantages of its parent company, Zhangyuan Tungsten, and years of accumulated product reputation, Achteck Tools will continue to work with global manufacturing partners — through independent innovation in cutting tool technology and professional service — to meet the challenges of machining difficult-to-cut materials.
AMB 2026 Stuttgart – International Metalworking Exhibition
Dates: September 15–19, 2026
Booth: Hall 3, 3E80
Venue: Messe Stuttgart, Germany
If you are looking for tooling solutions for superalloys, titanium alloys, or other difficult-to-machine materials, or if you wish to optimize existing processes and reduce overall manufacturing costs, we warmly welcome you to visit us at Hall 3, Booth 3E80.